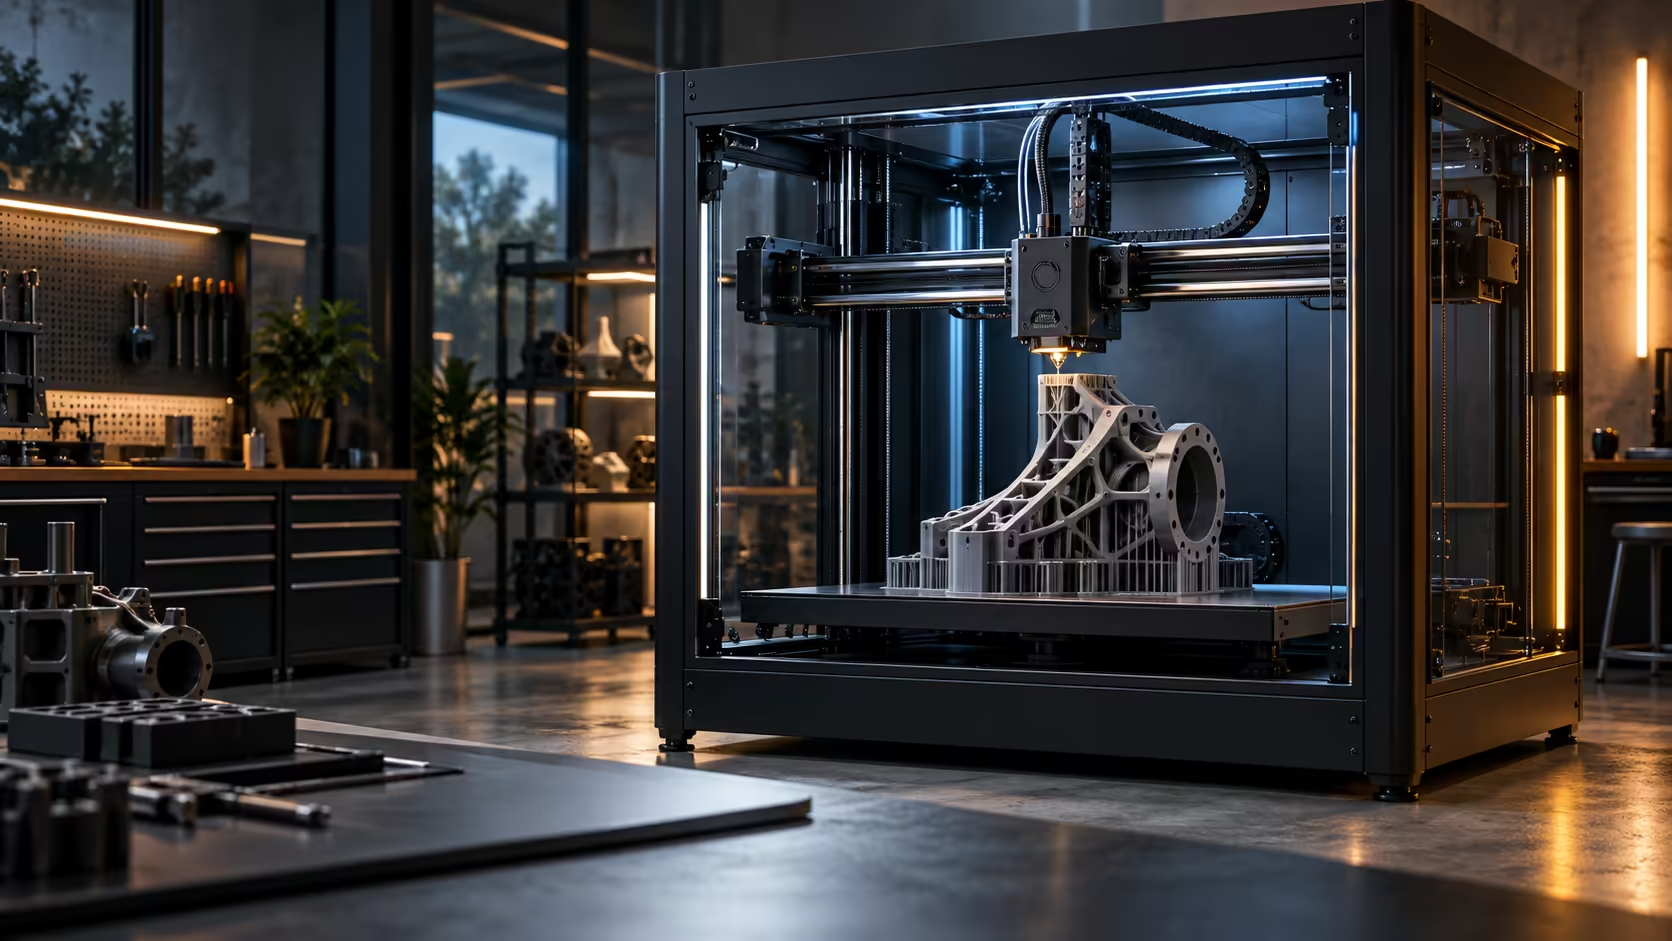
Two numbers on a spec sheet rarely get explained together properly, even though neither one really means much at all without the other sitting right beside it. 600mm/s printing paired with 20000mm/s2 acceleration is the combination that actually decides how a machine performs, not either figure read alone.
Quick Answer
Top speed is a ceiling that only matters on long, uninterrupted moves; acceleration is how quickly the toolhead reaches any speed at all, and it governs almost every short move in a typical print. A 30mm feature at 20000mm/s2 peaks at roughly 380mm/s regardless of what the top speed reads, because there simply is not enough distance to accelerate further before it is time to slow down again. This is exactly why the Creality K1 Max quotes the two figures together rather than leading with one alone, at R13,999.
📊 Working through the maths on a short move
Acceleration determines how much distance is needed to reach a given speed, and that distance grows with the square of the speed you are aiming for. On a 30mm feature, a printer running 20000mm/s2 spends most of that short distance still speeding up, tops out somewhere around 380mm/s, then immediately needs to start slowing down for whatever comes next.
This is not a flaw in the machine, it is simply how physics works on short segments, and it holds true regardless of which printer you are comparing.
📏 When 600mm/s actually shows up
Long, straight moves over 100mm are where top speed gets a real chance to matter: wide open infill, a long travel move across an empty bed, or a large flat surface printed in one continuous pass. These are exactly the moves where surface finish and accuracy are least critical, which is a convenient coincidence rather than a coincidence at all, since it is safe to run fast precisely where nobody is checking the result closely.
🧾 Reading a spec sheet with both numbers in mind
Judge a printer by how it actually performs on the kind of parts you regularly make, not by its top speed figure taken in isolation. A model covered in small features spends nearly all of its time in the acceleration phase and barely ever touches its rated top speed at all, while a model with long, open sections genuinely benefits from both numbers working together.
Print a small test object with a mix of short segments and one long straight wall to see this trade-off for yourself, and check filament flow characteristics too, since even strong acceleration and speed figures are capped by how fast a given material can actually melt and extrude. A case fan upgrade around the printer's location can help keep ambient temperature stable during long, fast prints, which supports consistent results at these speeds.
📐 A worked example with real numbers
Take a 40mm bracket wall and a machine running 20000mm/s2 of acceleration. Reaching 600mm/s from a complete standstill needs roughly 9mm of travel, and slowing back down again needs the same distance once more, which together already exceeds the entire 40mm segment before top speed is ever sustained for more than a passing instant. The printer spends effectively the whole wall accelerating and decelerating, never cruising.
Now take a much longer 400mm travel move across an open bed on that same machine. The same 9mm needed to reach 600mm/s is a genuinely small fraction of the total distance, so the toolhead cruises comfortably at full speed for the remaining 380-plus mm, and total time ends up dominated by that top speed figure rather than the acceleration rating at all. The same two numbers, on the exact same machine, decide the outcome completely differently depending purely on how long each individual move in the model actually happens to be.
🧮 Estimating your own print time more accurately
Slicers already run this exact calculation per individual move, but understanding it helps explain why a slicer's own time estimate sometimes disagrees sharply with a naive back-of-envelope calculation based on top speed alone. A model with an average segment length under 20mm behaves almost entirely as an acceleration-bound print regardless of its rated top speed, while a model built from long, sweeping curves and open infill approaches its top speed far more often.
Check your own typical models against this 20mm rule of thumb before assuming a headline speed figure predicts your real print times, since the gap between the two can run to several hours on a genuinely detailed part. Weigh acceleration figures from the 3D printer range against your own typical segment lengths rather than ranking machines purely by top speed alone.
Frequently Asked Questions
Which number matters more, top speed or acceleration?
Acceleration, for the vast majority of real prints, since short, fiddly features rarely get anywhere close to top speed at all in the brief distance available before the next corner arrives.
Can two printers with the same top speed perform very differently?
Yes, if their acceleration figures differ significantly, since acceleration decides how much of that top speed a typical print ever actually reaches.
Does a longer print always benefit more from high top speed?
Only if it contains long, uninterrupted moves; a long print made of many short features behaves the same as a short one in this respect.
Is there a real-world downside to very high acceleration?
It demands more from the frame and motion system to avoid shaking the model, which is why acceleration and frame rigidity are usually engineered together.
How far does a printer actually travel while reaching 600mm/s?
Roughly 9mm at 20000mm/s2 of acceleration, which is why any segment shorter than that distance never reaches the rated top speed at all before it needs to slow back down again.
Is a slicer's time estimate more reliable than a manual calculation?
Generally yes, since a slicer accounts for acceleration on every single individual move in the model, which a simple top-speed-based estimate ignores completely and entirely.
Does average segment length vary a lot between different kinds of models?
Considerably; mechanical parts with many small features often average well under 20mm per segment, while organic or architectural models with long, sweeping curves and open surfaces average much longer, sometimes past 100mm without a single sharp direction change.
Comparing printers by top speed alone?
Check the acceleration figure too, since it decides how much of that speed a real print actually uses.