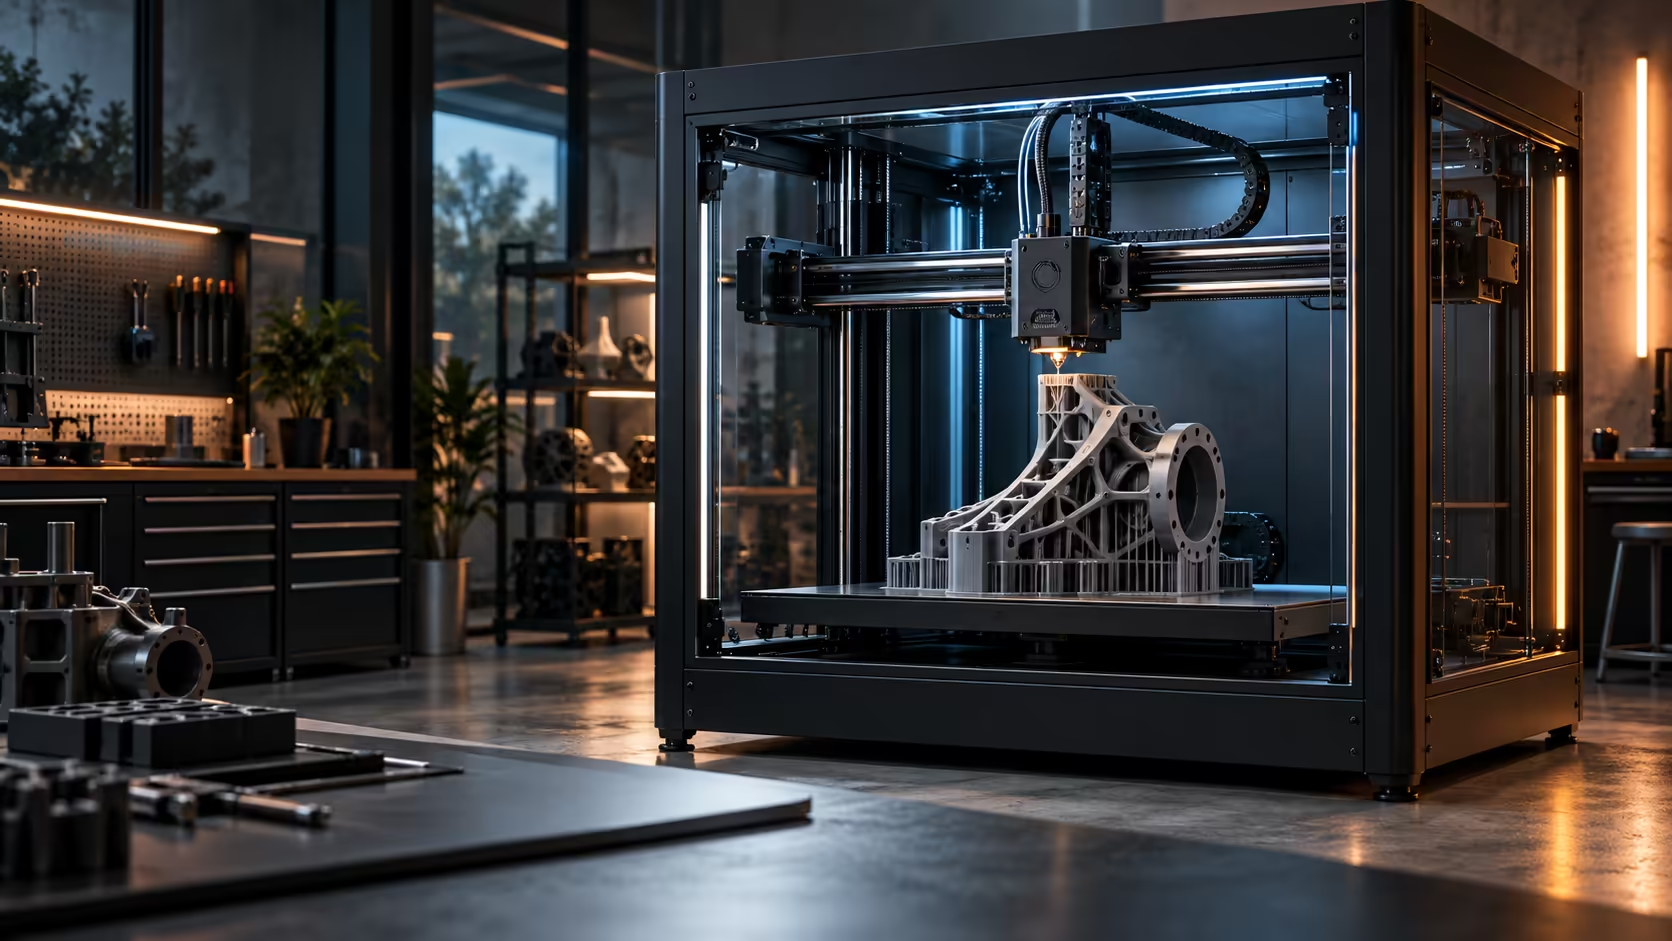
A spec sheet quoting 600mm/s and a print that visibly never gets there are not a contradiction, they are how real prints work. 3D printer speed on a data sheet describes a ceiling the toolhead is capable of, not a speed every model actually reaches.
Quick Answer
Flow rate, part cooling, corner acceleration and the model's own geometry all cap real speed long before the motor does. Melting plastic at 32mm3/s is the hard limit on the Creality K1 Max, and a 0.4mm line at 600mm/s needs more flow than that to keep up, so the printer runs wide lines fast and fine, detailed lines considerably slower. At R13,999, that trade-off is deliberate rather than a shortfall.
🌡️ Flow rate is the ceiling nobody quotes on the box
Speed and line width together determine how much plastic per second the hotend needs to melt and push out, and that number has a hard limit regardless of how fast the motors can move. At 0.4mm line width and standard layer height, reaching 600mm/s would demand more molten plastic per second than 32mm3/s of flow can supply.
The printer's firmware caps speed on thin lines accordingly, which is not a fault, it is the flow limit doing its job rather than under-extruding a line that looks fine but is actually starved of plastic.
🌬️ Part cooling sets its own limit
Even with enough flow, a line laid down too fast on a small feature has no time to solidify before the next pass arrives on top of it or beside it. Overhangs, bridges and small vertical features all need part-cooling fans running near 100%, and there is a speed past which no amount of fan airflow keeps up, so the slicer slows those specific moves down to well under 100mm/s regardless of the printer's rated top speed.
📐 The model itself is often the real limit
Short segments, tight corners and small holes rarely give the toolhead enough distance to reach top speed before needing to slow down again for the next feature. A model covered in detail behaves like a series of short moves regardless of what a benchmark test using long straight lines would suggest, which is why two prints on the same machine can finish at very different effective speeds.
Choose wide lines and thicker layers deliberately when a part does not need fine detail, since that is the setting combination that actually lets flow rate and top speed align, rather than fighting each other. Browse the 3D printer range with flow rate specifically in mind rather than the headline speed figure, stock filament suited to faster printing, and consider slicer software with good adaptive speed control if a model's own geometry keeps forcing unwanted slowdowns.
Frequently Asked Questions
Is 600mm/s achievable on every print?
No, only on long, wide-line moves where flow rate and cooling can both keep up; fine detail and small features run considerably slower.
Does a higher flow rate always mean faster prints?
Only on wide lines that actually need that much plastic per second; fine, detailed work is limited by cooling and geometry rather than flow.
Why does the printer slow down on small features automatically?
Cooling and flow both have limits that small features hit before top speed does, so the firmware or slicer reduces speed to keep the print from failing.
Can changing line width improve real print speed?
Yes, wider lines carry more plastic per pass, which lets a printer approach its rated top speed more often on parts that do not need fine detail.
Wondering why your printer never hits its rated top speed?
Check flow rate and cooling limits before assuming the machine is underperforming.