
PCIe 5.0 vs PCIe 4.0 for Video Editing in 4K in SA
PCIe 5.0 and PCIe 4.0 differ most in lane support, compatibility, and upgrade value for video editing in 4k. SA buyers should match the choice to their actual hardware and games.
Read moreFor Achieving 600mm/s Print Speeds With, 600mm/s speed is the detail to verify first. The safer buy is the one where achieving 600mm/s print speeds with high-flow petg on lines up with material storage, slicer profile and calibration.
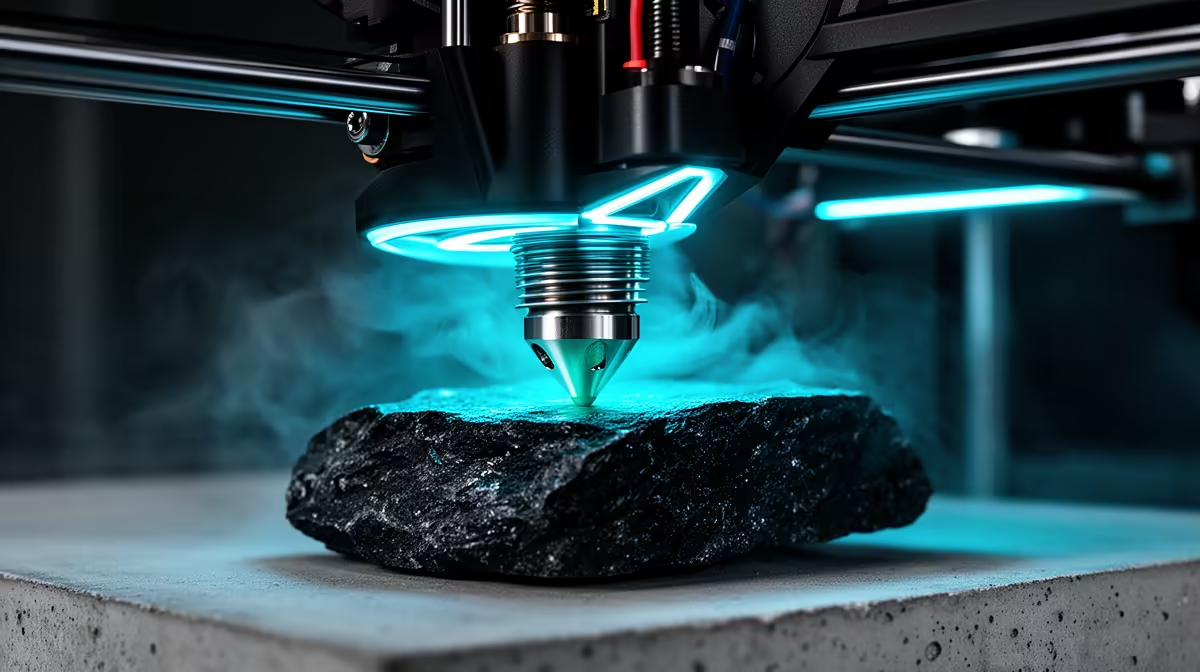
Getting achieving 600mm print 3D printer right is mostly about the first practical setup pass. Confirm 600 mm print-speed planning, make standard filament diameter easy to manage, and keep diameter tolerance check visible for small workshop use.
The practical answer for achieving 600 mm/s Print Speeds With High-Flow PETG on Standard FDM Printers is to match 600 mm print-speed planning, standard filament diameter and diameter tolerance check to your main device or workspace first. A practical shortlist for achieving 600mm print 3D printer should reduce resin handling mistakes before the compatibility pass ends.
Use one normal session as the test case for achieving 600 mm/s Print Speeds With High-Flow PETG on Standard FDM Printers. During small workshop use, watch how 600 mm print-speed planning affects timing, handling or comfort, then compare standard filament diameter against the product you use most. If resin handling mistakes is the concern, check diameter tolerance check on achieving 600mm print 3D printer in the upgrade pass. The useful sign for achieving 600mm print 3D printer is repeatable cleaner surfaces after the battery pass.
Build quality for achieving 600 mm/s Print Speeds With High-Flow PETG on Standard FDM Printers is the way the details hold up under ordinary use. For achieving 600mm print 3D printer, confirm 600 mm print-speed planning in the setup pass. Confirm diameter tolerance check, then check whether 600 mm print-speed planning and standard filament diameter still make sense when the product is packed away, moved or shared. For achieving 600 mm/s Print Speeds With High-Flow PETG on Standard FDM Printers, a cleaner routine is stronger evidence than louder wording.
The final check for achieving 600 mm/s Print Speeds With High-Flow PETG on Standard FDM Printers is whether you can explain the benefit in one real situation. If the answer is small workshop use, connect it directly to 600 mm print-speed planning, standard filament diameter or diameter tolerance check. If resin handling mistakes is the concern, check diameter tolerance check on achieving 600mm print 3D printer in the support pass. For achieving 600mm print 3D printer, confirm 600 mm print-speed planning in the signal pass.
600 mm s Print Speeds With High-Flow PETG on Standard FDM Printers still feels confusing, remove any Achieving 600mm Print option that does not explain 600 mm print-speed planning or standard filament diameter plainly.
Start with 600 mm print-speed planning, then check standard filament diameter and diameter tolerance check on the device or workspace you use most. That gives achieving 600 mm/s Print Speeds With High-Flow PETG on Standard FDM Printers a practical test before style.
Test achieving 600mm print 3D printer in small workshop use during the week-one pass. The useful sign for achieving 600mm print 3D printer is repeatable cleaner surfaces after the comfort pass.
Use standard filament diameter as the layout pass tie-breaker for achieving 600mm print 3D printer. Achieving 600 mm/s Print Speeds With High-Flow PETG on Standard FDM Printers should fit high-detail models as well as the main use case.
A hardened steel or copper alloy high-flow nozzle of 0.6mm or 0.8mm diameter is essential for sustained 600mm/s PETG without clogging or grinding.
Yes. At 600mm/s the nozzle dwell time per layer is very short. An enclosure at 40-50 degrees Celsius prevents delamination and maintains 85-90% part strength.
High-flow PETG hotends use a hardened 60W or 80W heater block that sustains 240-250 degrees Celsius under constant 15-20 gram-per-minute extrusion demand.
0.3mm layers with 25-30% gyroid infill at 600mm/s maintain 80% of the tensile strength of slower prints while reducing print time by 60-70%.
Input shaping is required. Without it, ringing artifacts appear on corners. Resonance calibration targets typically fall at 30-55Hz for PETG at 600mm/s.
Bambu Lab A1 and X1 series are factory calibrated for 500-600mm/s PETG. Stock Ender-3 printers cap at 150-200mm/s without significant hardware modification.
PCIe 5.0 and PCIe 4.0 differ most in lane support, compatibility, and upgrade value for video editing in 4k. SA buyers should match the choice to their actual hardware and games.
Read more
ATX 3.1 and ATX 3.0 differ most in connector handling and GPU power design. For SA gamers, the choice comes down to your graphics card, PSU quality, cable clearance, and whether a newer 12V-2x6-ready unit makes sense for the build.
Read more
80+ Platinum or 80+ Titanium for cinematic should be shortlisted around the job it must do. South African buyers should compare fit, performance, compatibility, and upgrade room, warranty path, and upgrade room before treating any pick as best.
Read more
AM5 and AM4 can both work for competitive esports, but the real-world difference is platform headroom. SA players should compare CPU choices, memory speed, latency goals, monitor refresh, and future upgrade plans.
Read more
LGA 1851 and LGA 1700 differ most in CPU support, compatibility, and upgrade value for couch co-op gaming. SA buyers should match the choice to their actual hardware and games.
Read more
DLSS 4 and DLSS 3 differ most in game support, compatibility, and upgrade value for streaming on twitch and youtube. SA buyers should match the choice to their actual hardware and games.
Read more
RTX 5090 on a 1200W PSU has usable headroom when the supply is strong and the build is measured. For SA gamers, OC potential depends on CPU draw, cooling, cabling, stability targets, and how much safety margin you keep.
How to fix low FPS on gaming laptop starts with power mode, drivers, heat, and game settings. Use this South Africa-focused checklist to confirm charger use, GPU selection, RAM pressure, and cooling before changing parts or tweaking every setting.
Real world difference between b850 b650 mmo live service games sits in stability, networking, storage, and upgrade room. SA players should compare LAN quality, USB layout, RAM support, and SSD slots for always-updated games.
Dead Pixel on Wi-Fi 7 Router is likely a display-path or source-title issue, so check the screen, cable, driver state, and related system symptoms before blaming the device itself.
Put the headphones in pairing mode, open Bluetooth and devices in Windows 11, then add the headset. If it fails, remove the old pairing and check charge, range and drivers.
Microsoft says upcoming Windows 11 work will target memory use on 8GB PCs and improve boot and sign-in responsiveness. There is no public release date or measured uplift yet.
Windows 11 does not show CPU temperature in its standard Settings pages. Use your CPU maker's supported utility or a trusted monitor, then read idle and loaded temperatures in context.
The Colorful MEOW X16 Pro pairs a Ryzen 7 8745HX with a 115W RTX 5060 Laptop GPU. It is a China-only launch for now, so local RTX 5060 pricing is the practical benchmark.
Industry reports point to another roughly 10 percent Intel processor increase from 5 October, but Intel has not published a consumer price list confirming the scope. South African buyers should treat it as a risk signal, not a guaranteed Rand change.
Tests reported audio capture and local-network scanning on a specific LG television with its screen off. LG says supported standby modes can keep voice and connected-device features active, so owners should review model-specific settings.
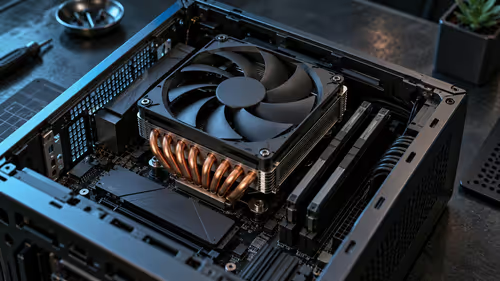
Thermalright's AXP120-X77 is a 77 mm top-down cooler with six heatpipes and a slim 120 mm fan. Local availability is not confirmed, so compact-PC builders should verify case height, memory clearance and socket support before comparing it with stocked coolers.
One-sided sound can come from balance settings, a dirty or loose connector, Bluetooth pairing data, firmware, the source device or a failed cable or driver. A short swap test isolates the cause before you reset software or replace the headset.