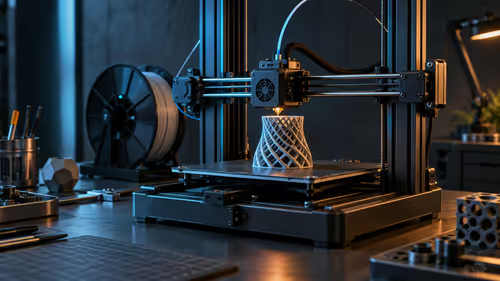
Levelling a print bed used to mean a piece of paper and a lot of patience, checking four corners by feel and hoping the middle was close enough. AI LiDAR replaces the feel with a light-based scan, and using it properly is a five-minute routine rather than a guess.
Quick Answer
Clean the plate, heat it to printing temperature, then run the automatic levelling routine so the sensor maps height across the full bed while it is actually in its working state. Follow that with a one-layer test patch to fine-tune Z offset by eye. On the Creality K1 Max, at R13,999, the LiDAR pass also reads the extruded line itself, which is what catches a first layer that is level but still under- or over-extruding.
📡 Run the scan hot, not cold
A bed expands as it heats, sometimes by more than the 0.1 to 0.2mm tolerance you are trying to hit, so a levelling pass done cold is measuring a shape the bed will not hold once printing starts. Heat the plate to a typical PLA or PETG working temperature of 50 to 70C and the nozzle to somewhere near 200C first, then start the levelling routine from the printer's Settings menu.
The scan builds a compensation mesh across the plate rather than checking four corners and assuming the middle follows. That mesh is what lets a wide bed stay level at the edges and the centre at once, which matters more as the plate gets bigger.
🧪 Fine-tune with a one-layer test, not a full print
Levelling gets you close; a Z offset test gets you correct. Print a single-layer square or the built-in test pattern and look at the line: too high and it looks stringy with gaps between passes, too low and it looks flattened with a raised ridge along the edge.
Adjust the offset in small steps, no more than 0.02mm at a time, and reprint the test patch rather than jumping straight to a full model. A first layer that looks slightly rough but fully adheres is closer to correct than one that looks glassy smooth but peels at a corner. Slicing software on the computer feeding the printer is where that first-layer speed and temperature actually get set, so a levelling pass only pays off if the profile matches the material going onto the plate.
🔍 What the second scan pass actually buys you
A touch probe only ever tells you where the bed physically is. LiDAR on the K1 Max goes a step further after the first layer is down: it reads the width of the line that was just extruded, not just the height of the plate under it, and flags a layer that is level but still printing too thin or too thick.
That second check is what separates a bed that measures level from a first layer that will actually hold for the next fourteen hours. If a print keeps failing despite a clean levelling pass, check flow rate next rather than repeating the same scan expecting a different result, and rule out a partially clogged nozzle too, since a restricted orifice can under-extrude even when the bed height reading comes back perfect. Browse the 3D printer range if a machine without this second check is the reason prints keep needing manual rescue, and keep filament sealed between sessions so flow stays consistent from one levelling pass to the next.
Frequently Asked Questions
Should I level the bed before every single print?
Not every print, but after moving the printer, swapping the plate, or if the last few first layers looked inconsistent.
What does a bad Z offset look like on the test patch?
Too high leaves visible gaps between lines; too low leaves a raised, flattened ridge where the nozzle scraped the plate.
Can software fix a bed that is physically warped?
A compensation mesh corrects for warping within a few tenths of a millimetre; a plate that is badly bent needs replacing, not calibrating around.
Is manual bed levelling still worth learning?
It is useful as a fallback and for understanding what the automatic pass is doing, but day to day the automatic routine is faster and more consistent.
How often does the compensation mesh need rebuilding?
Whenever the bed surface itself changes meaningfully, a new build plate fitted, a bent corner straightened out, or a printer that has been relocated to a different bench entirely, since the old mesh was measuring a surface that no longer matches the current one.
Does a clean scan guarantee a clean first layer every time?
No, a level, well-scanned bed still needs the right nozzle temperature and flow for the specific material loaded; scanning fixes the geometry of the surface, not the settings that govern how much plastic actually reaches the plate once printing starts.
Tired of babysitting the first layer of every print?
Run the hot levelling pass properly once, then trust the mesh it builds.